
 中文简体
 English
 русский
 Inquiry
Don't hesitate to send a message
I. Introduction: Solving the "Impossible" Task The phrase "fitting a square peg into a round hole" is a universal symbol...
READ MOREThree suppliers will give you three different answers about the best material for drill bits: high-speed steel, cobalt, or solid carbide. All three answers are correct, but each is correct only inside a narrow set of conditions, a workpiece grade, a hole diameter, a machine, and a target number of holes.
Get the match wrong and the cost appears fast. A 6 mm HSS M2 bit running dry in 304 stainless at 1,400 rpm usually dulls inside 15 to 25 holes, while the same bit in low-carbon steel lasts for hundreds. Moving that stainless job to an M35 cobalt bit multiplies tool life by roughly three for about twice the unit price, which is why material selection belongs to procurement as much as to the tool crib.
The rest of this guide follows that order, because the three material families behave very differently once heat, abrasion and impact enter the cut.
Content
The short answer: wood is drilled with high-carbon steel or HSS, mild steel with HSS M2, stainless and alloy steel with cobalt M35 or M42, high-volume metal work with solid carbide, and concrete only with carbide-tipped SDS tooling.
| Material | Heat limit | Best workpiece fit | Relative price |
| HSS M2, bright finish | 540-600 C | Mild steel, aluminium, wood, plastics | 1.0x |
| HSS M2 with TiN coating | 540-600 C | Sheet metal, general repair, maintenance kits | 1.2-1.5x |
| Cobalt M35 or M42 | 600-650 C | Stainless 304 and 316, alloy steel, titanium | 2.0-2.8x |
| Carbide-tipped steel body | 800 C and above | Concrete, brick, block, abrasive sheet goods | 3-5x |
| Solid carbide | 1,000 C and above | CNC metal work, composites, high volume runs | 6-10x |
Standard brad-point wood bits come in high-carbon steel and in HSS, and the real difference is repetition, not sharpness. High-carbon steel takes a keen edge cheaply and suits cabinet work and site carpentry where a bit is used a few times a week. HSS holds that edge through abrasive sheet goods such as MDF and particleboard, where glue lines and mineral filler dull a soft steel edge inside a single shift. Auger bits and forstner bits follow the same rule: carbon steel for occasional deep boring, HSS for repeat production.
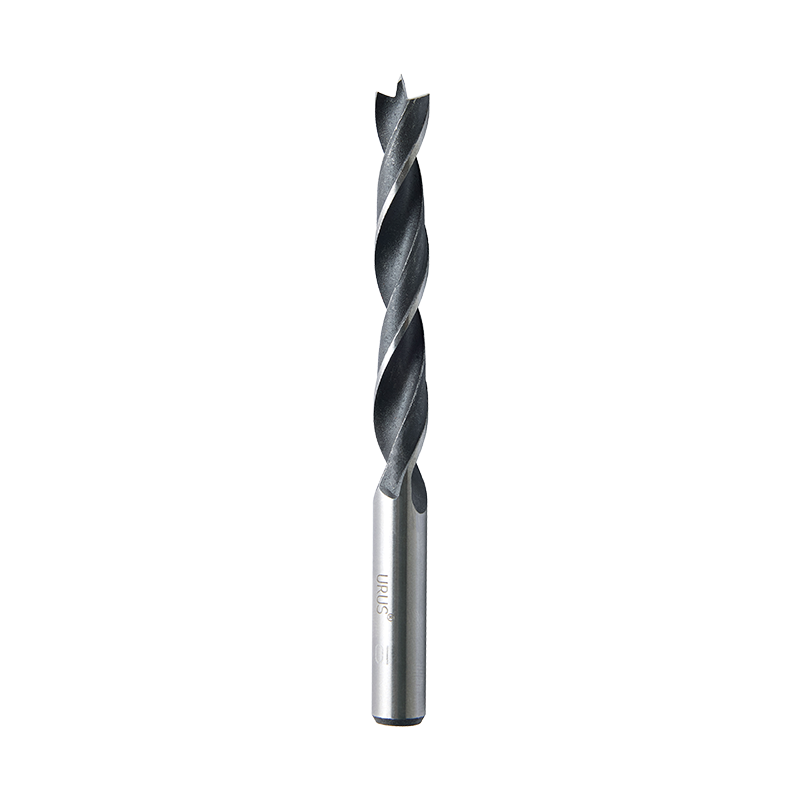 Standard Brad Point Wood Drill Bit for Accurate Wood DrillingA wood drill bit with a precision center point and round shank, suited to accurate positioning and standard chucks for general wood drilling.View Product →
Mild steel, aluminium, brass and plastics are drilled most economically with HSS M2, usually at a 118-degree point for general work and a 135-degree split point when the bit has to hold a marked centre without walking. Stainless 304 and 316 work-harden under a dull edge, so the tool has to cut rather than rub: cobalt M35 or M42 with a split point keeps the edge alive long enough to finish the hole. A pilot point geometry helps on curved and thin sections. Solid carbide only enters when volume, rigidity and coolant control are all in place.
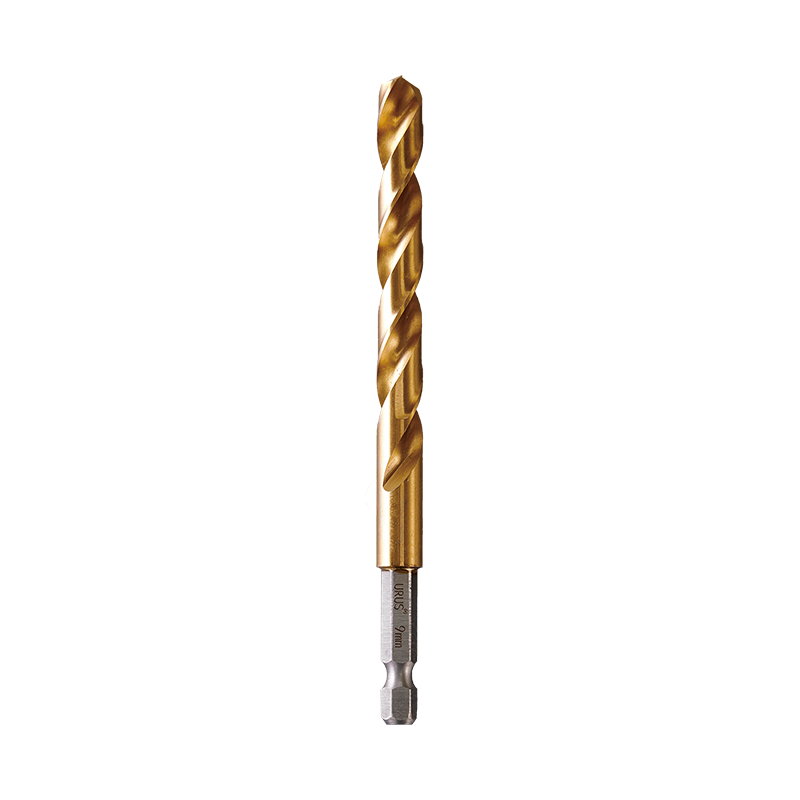 Custom Split Point Metal Drill Bit for Quick-Change ChucksA metal drilling bit with split point geometry and multiple finish options, designed for 1/4-inch quick shank chucks and diameters from 1.0 to 13.0 mm.View Product →
No cobalt or HSS bit belongs in concrete. Hammer drilling applies impact loading and mineral abrasion at the same time, so the cutting edge has to be tungsten carbide brazed into a steel body. SDS-plus covers roughly 4 to 16 mm holes in brick, block and standard concrete, while SDS-max takes larger diameters and heavier reinforcement work. A three-cutter carbide head centres faster on uneven surfaces and reduces the walking that ruins hole position on a rough wall.
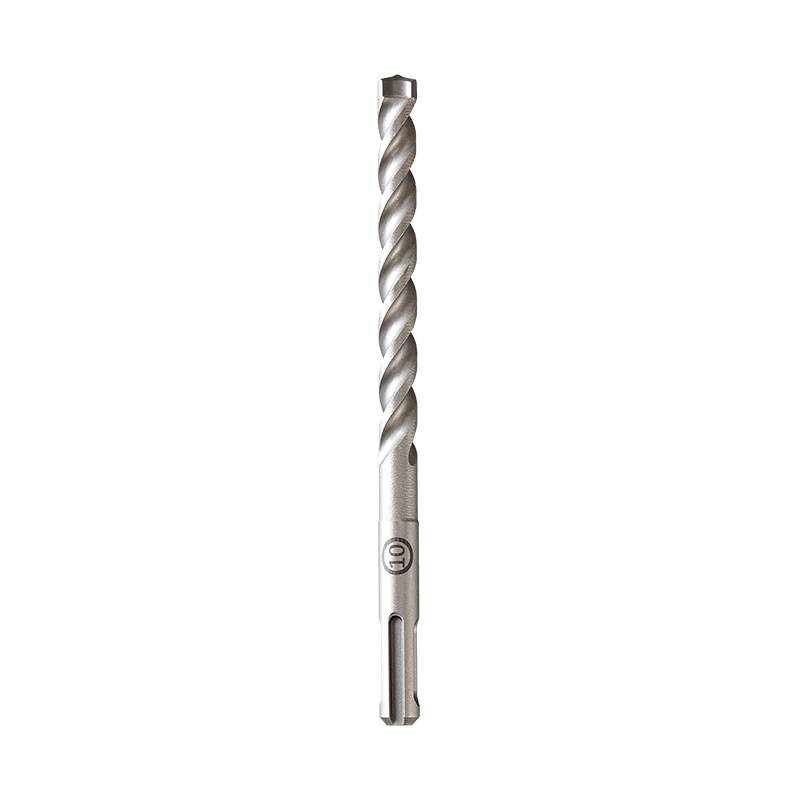 Custom SDS-3-Cutter Carbide-Tipped Hammer Drill Bit for MasonryA masonry hammer bit with a three-cutter carbide tip and hardened chrome-vanadium body, intended for drilling bricks, concrete, and stone across multiple sizes.View Product →
Point geometry, flute count and shank standard matter as much as the base material, so keep a reference for drill bit types and their uses beside your material specification when you write a purchase brief.
Most specification errors we see in quotations come from four misunderstandings about what a bit is actually made of.
Red hardness is the temperature at which a cutting edge softens and stops cutting cleanly. HSS M2 holds its edge to roughly 540-600 C, cobalt grades push that to about 600-650 C, and carbide keeps cutting well beyond that, which is the entire reason cobalt and carbide exist as separate price tiers.
In 304 stainless, M35 cobalt commonly returns about three times the holes of HSS M2, and carbide-tipped geometry returns more than five times, enough to lower cost per hole even though the unit price is higher.
The arithmetic is straightforward. An HSS M2 bit at $3.00 that produces 20 holes costs $0.15 per hole. A cobalt bit at $7.50 that produces 60 holes costs $0.125 per hole, and it also removes two bit changes from the operator's shift. On a cell drilling 600 stainless holes a day, that difference removes roughly 20 tool changes every day.
A drill bit specification is complete only when it names the workpiece, the hole, the machine, the expected life and the verification method. Anything less leaves the material choice to your supplier's assumption.
Suppliers who build bits for OEM programmes usually welcome that level of detail, because it removes argument later. Zhejiang URUS Tools Co., Ltd., which manufactures drill bits, pliers and hand tool sets in Jiashan, Zhejiang under the Bison brand, works across wood, metal and masonry lines with ISO9001:2015 certification, a national high-tech enterprise designation, and a TUV Rheinland cooperation test laboratory established in 2017. Buyers preparing a wider brief can start from this overview of cutting bits for drills: types, materials and how to choose.
No. Cobalt buys hot hardness and abrasion resistance and gives up some toughness in return, at two to three times the unit price. In wood, mild steel, aluminium and general maintenance work, HSS M2 is the better economic choice. Cobalt earns its premium when the workpiece is stainless, alloy steel above roughly 30 HRC, or titanium, or when edge temperature is the factor limiting tool life.
No. Titanium nitride is a coating of roughly 1 to 4 microns on the same HSS substrate. It lowers friction, improves chip flow and slows flank wear, but the base steel still determines how much heat the edge survives before it softens.
Tungsten carbide. Concrete is drilled with impact, so the tip must be a brazed carbide insert mounted in an SDS-plus or SDS-max shank. HSS and cobalt edges fail quickly under that combination of hammering and mineral abrasion.
Compare cost per hole at a fixed workpiece, diameter and speed. Ask for hardness data, tip runout figures, coating thickness and a sample batch tested on your own machine before releasing a container order, and keep that test result attached to the specification.
I. Introduction: Solving the "Impossible" Task The phrase "fitting a square peg into a round hole" is a universal symbol...
READ MOREMetalworking has always been a cornerstone of industrial development, shaping everything from automotive components to a...
READ MORE1. What Are Waterpump Pliers? – The Flexible “All-Rounder” Tool In modern industrial manufacturing and daily maintenance...
READ MORESelecting the appropriate industrial cutting tools is a critical decision that directly impacts manufacturing efficiency...
READ MORE
+86-573-84611229

+86-573-84611518


NO.35 Yucao Road, Ganyao Town, Jiashan City, Zhejiang Province, China
